Industrial-grade AC & DC geared motors engineered for automation, robotics, conveyors, and heavy industrial machinery.
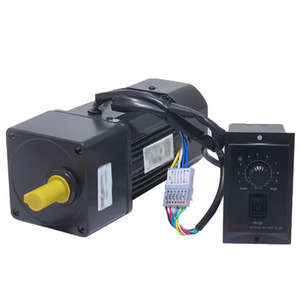
Comprehensive insights into compliance architecture, mechanical power transmission dynamics, and total cost of ownership (TCO) optimization.
In global industrial motion control, the CE Marking (Conformité Européenne) is not merely a trading passport—it is an auditable verification of structural safety, electromagnetic compatibility, and energy efficiency compliance. Original Equipment Manufacturers (OEMs) and plant infrastructure directors importing gear motors into the European Economic Area (EEA) or regulated international jurisdictions must navigate rigorous safety directives.
A authentic CE-certified gear motor must satisfy three foundational European Union Directives:
Working with certified gear motor factories ensures every unit undergoes rigorous Type-Tested Assemblies (TTA), dielectric strength testing, insulation resistance checking, and acoustic noise spectrum analysis before factory acceptance sign-off.
Selecting the optimal gear motor topology requires evaluating torque density, mechanical backlash tolerances, thermal dissipation capacity, and radial load ratings. Below is a comparative engineering breakdown of the dominant gear motor designs produced by premier manufacturing facilities:
| Gear Architecture | Typical Efficiency | Backlash Range | Torque Density | Primary Application Profile |
|---|---|---|---|---|
| Planetary Gearbox (AC/BLDC) | 92% - 97% | ≤ 3 - 12 arcmin | Ultra-High | Robotics, Servo Positioning, AGVs, High-Precision CNC |
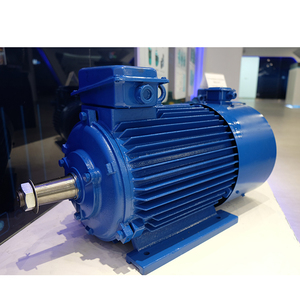
| Helical Gear Reducer (R/K/F Series) | 94% - 98% | ≤ 15 - 25 arcmin | High / Heavy Duty | Conveyor Systems, Water Pumps, Metallurgy, Mixers |
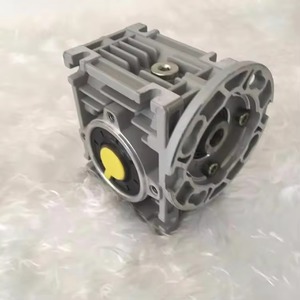
| NMRV Worm Gearbox | 65% - 88% | ≤ 30 - 50 arcmin | Moderate / Self-Locking | Smart Home Gates, Packaging Belts, Small Hoists |
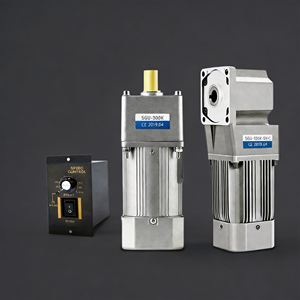
| Right-Angle Helical-Bevel | 90% - 95% | ≤ 10 - 18 arcmin | High / Compact | Intralogistics Sorting, Bottling Lines, Cleanrooms |
To maximize service life (L10 bearing life exceeding 20,000 hours), motor winding insulation should meet or exceed Class F (155°C) thermal rating with Class H varnish impregnation, paired with IP65 or IP67 enclosure seals to withstand wet washdown environments.
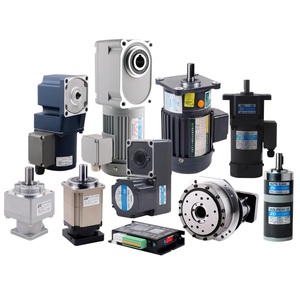
Our engineered power transmission products integrate cutting-edge metallurgy, precision CNC gear hobbing, and automated stator winding.
Carburized alloy steel gears (20CrMnTi) hardened to HRC 58-62. Precision tooth grinding achieves DIN Class 5-6 accuracy for whisper-quiet vibration levels (<62 dBA).
Custom-engineered low-loss silicon steel laminations and high-purity copper windings minimize eddy current losses, cutting plant electricity costs by up to 18% annually.
100% of manufactured gear motors undergo automated surge testing, dynamic balancing, oil seal leak check under pressure, and temperature rise verification under full rated load.
Extensive modularity supporting IEC standard B5/B14 flanges, dual-output shafts, stainless steel shafts, keyless locking elements, and customized speed ratios (1:3 to 1:3000).
Optional onboard smart drive modules with CANopen, Modbus RS485, or EtherCAT support. Embedded vibration and thermal sensor ports enable Industry 4.0 predictive maintenance.
Every shipment is delivered with comprehensive documentation including CE Declarations of Conformity, ROHS compliance reports, ISO 9001 factory audits, and factory test sheets.
Key market vectors shaping the future of global industrial drive procurement through 2030.
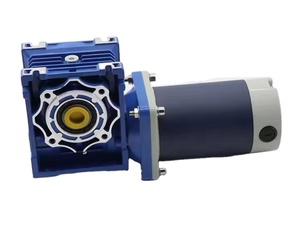
While traditional induction gear motors remain workhorses for continuous-duty pumping and general conveyor operations, procurement managers are increasingly shifting toward Permanent Magnet Brushless DC (BLDC) and Permanent Magnet Synchronous Motors (PMSM). Driven by rising energy tariffs globally, PMSM gear motors offer uniform torque over wide speed ranges without efficiency drop-offs at partial load conditions. In automated guided vehicles (AGVs) and warehouse robotics, 24V/48V low-voltage BLDC planetary gear motors deliver high power density within compact wheel hubs.
The legacy model of reactive drive maintenance is rapidly disappearing. Procurement guidelines for tier-1 automotive manufacturing plants now mandate gear motors equipped with integrated vibration accelerometers, winding thermistors (PT100/PTC), and current monitoring telemetry. Connecting gear motor telemetry directly to SCADA edge controllers enables maintenance teams to detect gear pitting, lubricant degradation, or bearing spalling weeks before unexpected line stoppage occurs.
With multinational corporations adopting strict Scope 3 emission reduction targets, gear motor factory audits now scrutinize manufacturing supply chains. Eco-friendly synthetic lubricants (biodegradable polyglycol oils), recycled copper stator wire sourcing, and ISO 14001 certified zero-waste manufacturing facilities are rapidly becoming prerequisites for securing long-term OEM supply agreements.
Engineered gear motor solutions tailormade for demanding operating environments worldwide.
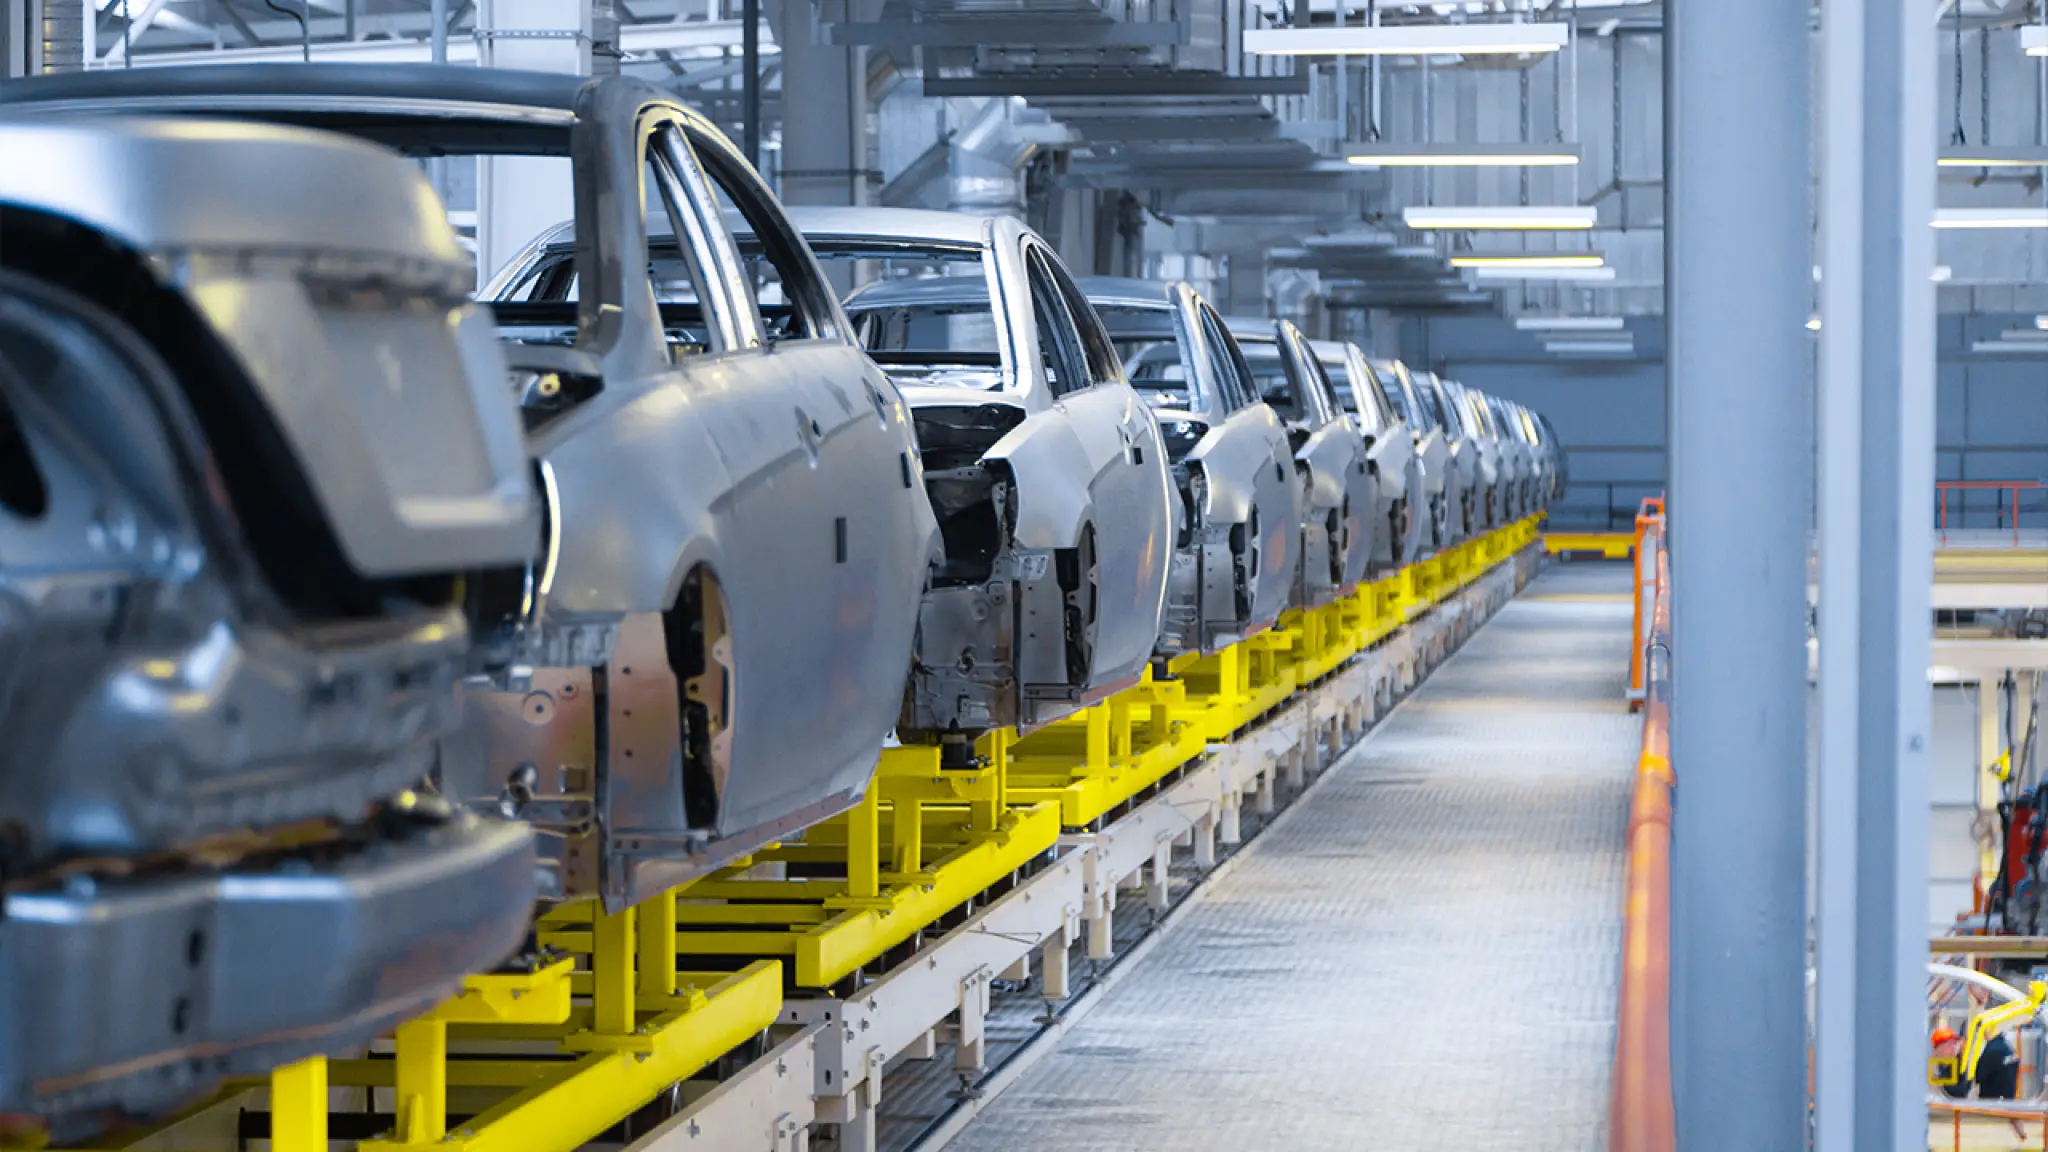
High-torque planetary and right-angle gear motors powering robotic transfer shuttles, welding positioners, and automated assembly stations requiring sub-millimeter positioning accuracy.
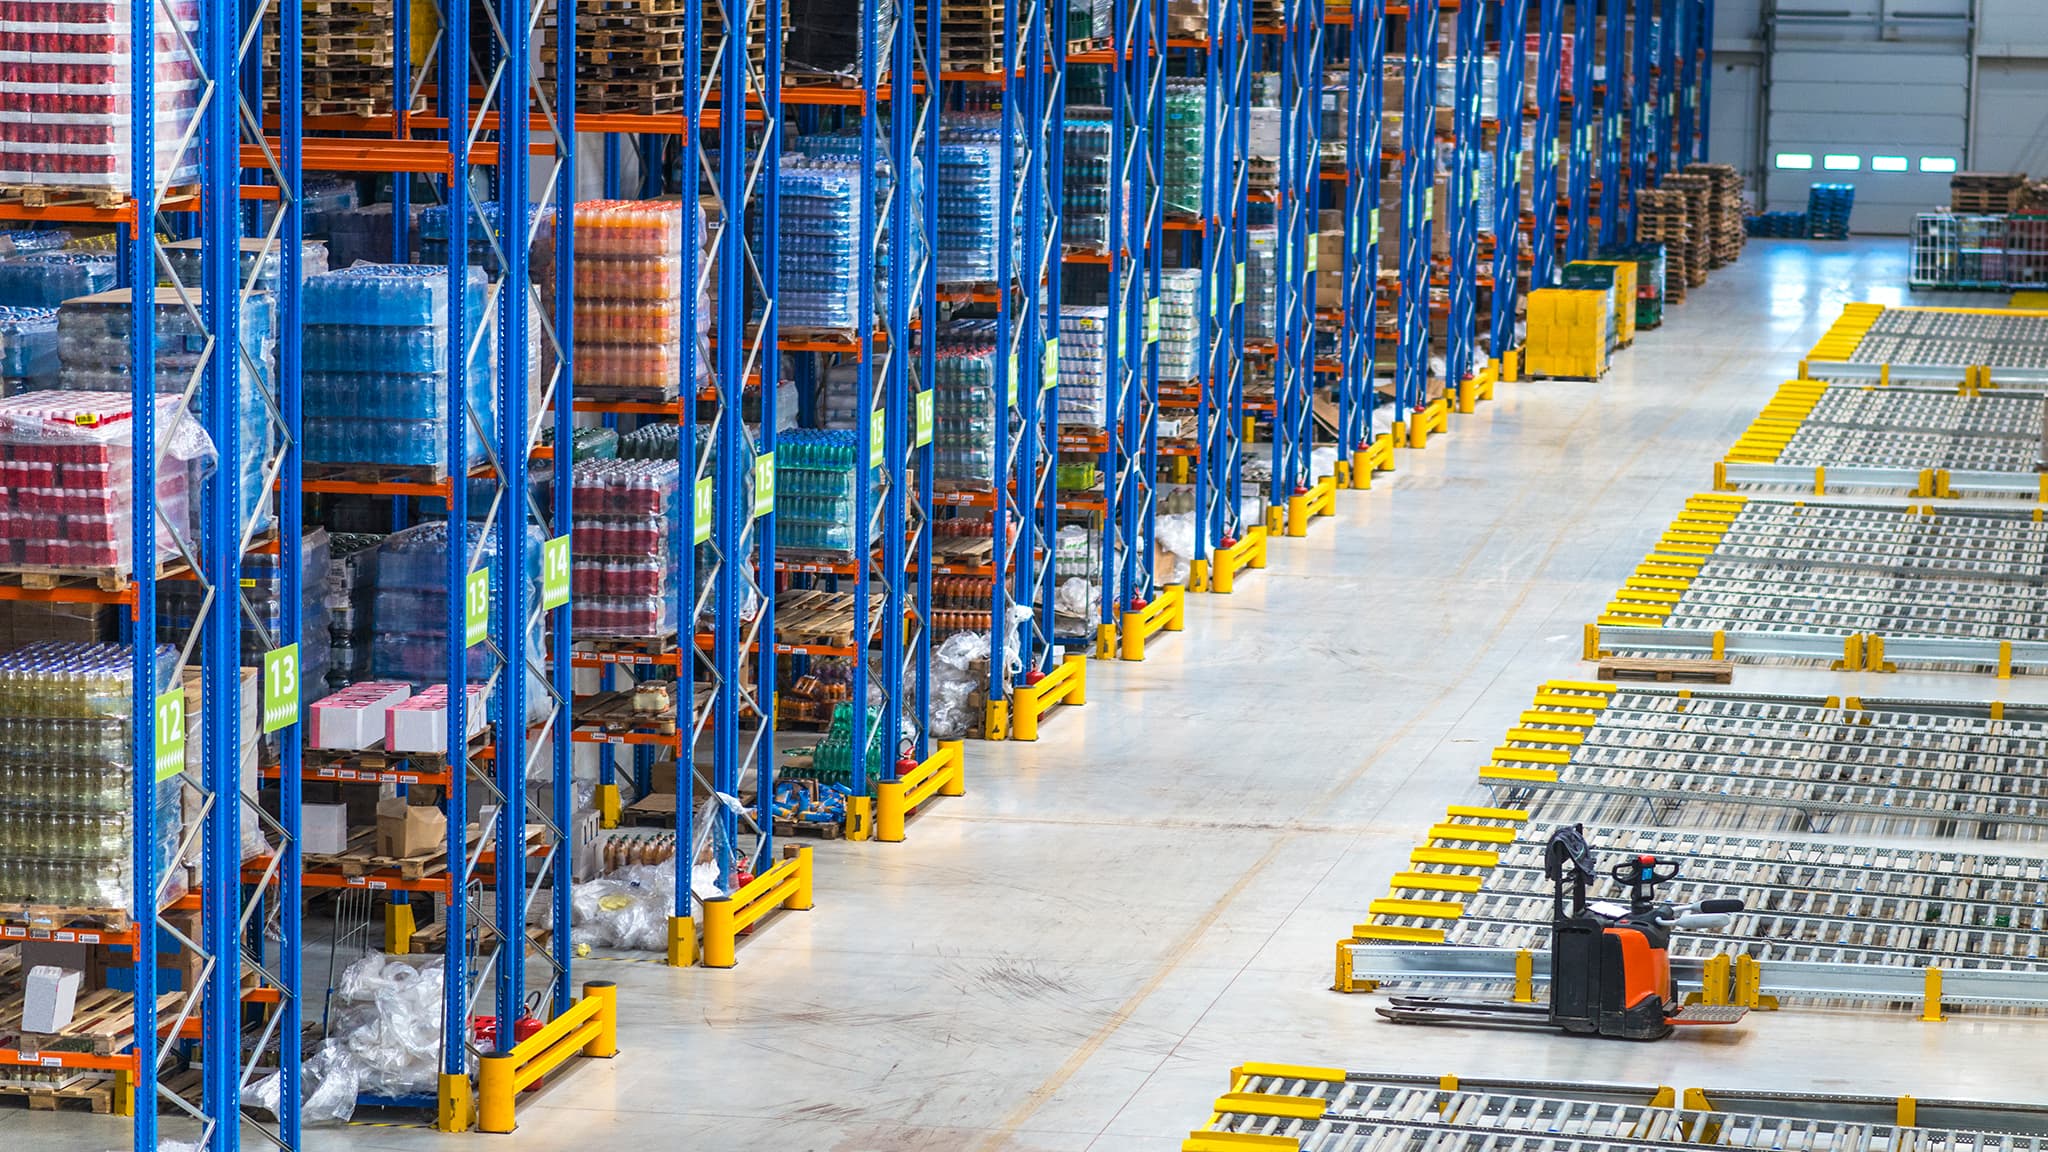
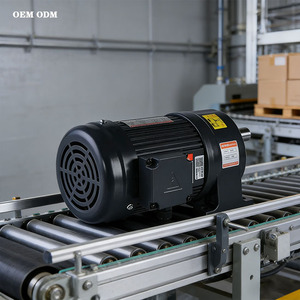
Compact 24V/48V DC gear motors integrated with high-speed roller conveyors, cross-belt sorters, and luggage handling systems operating 24/7 under continuous duty cycles.
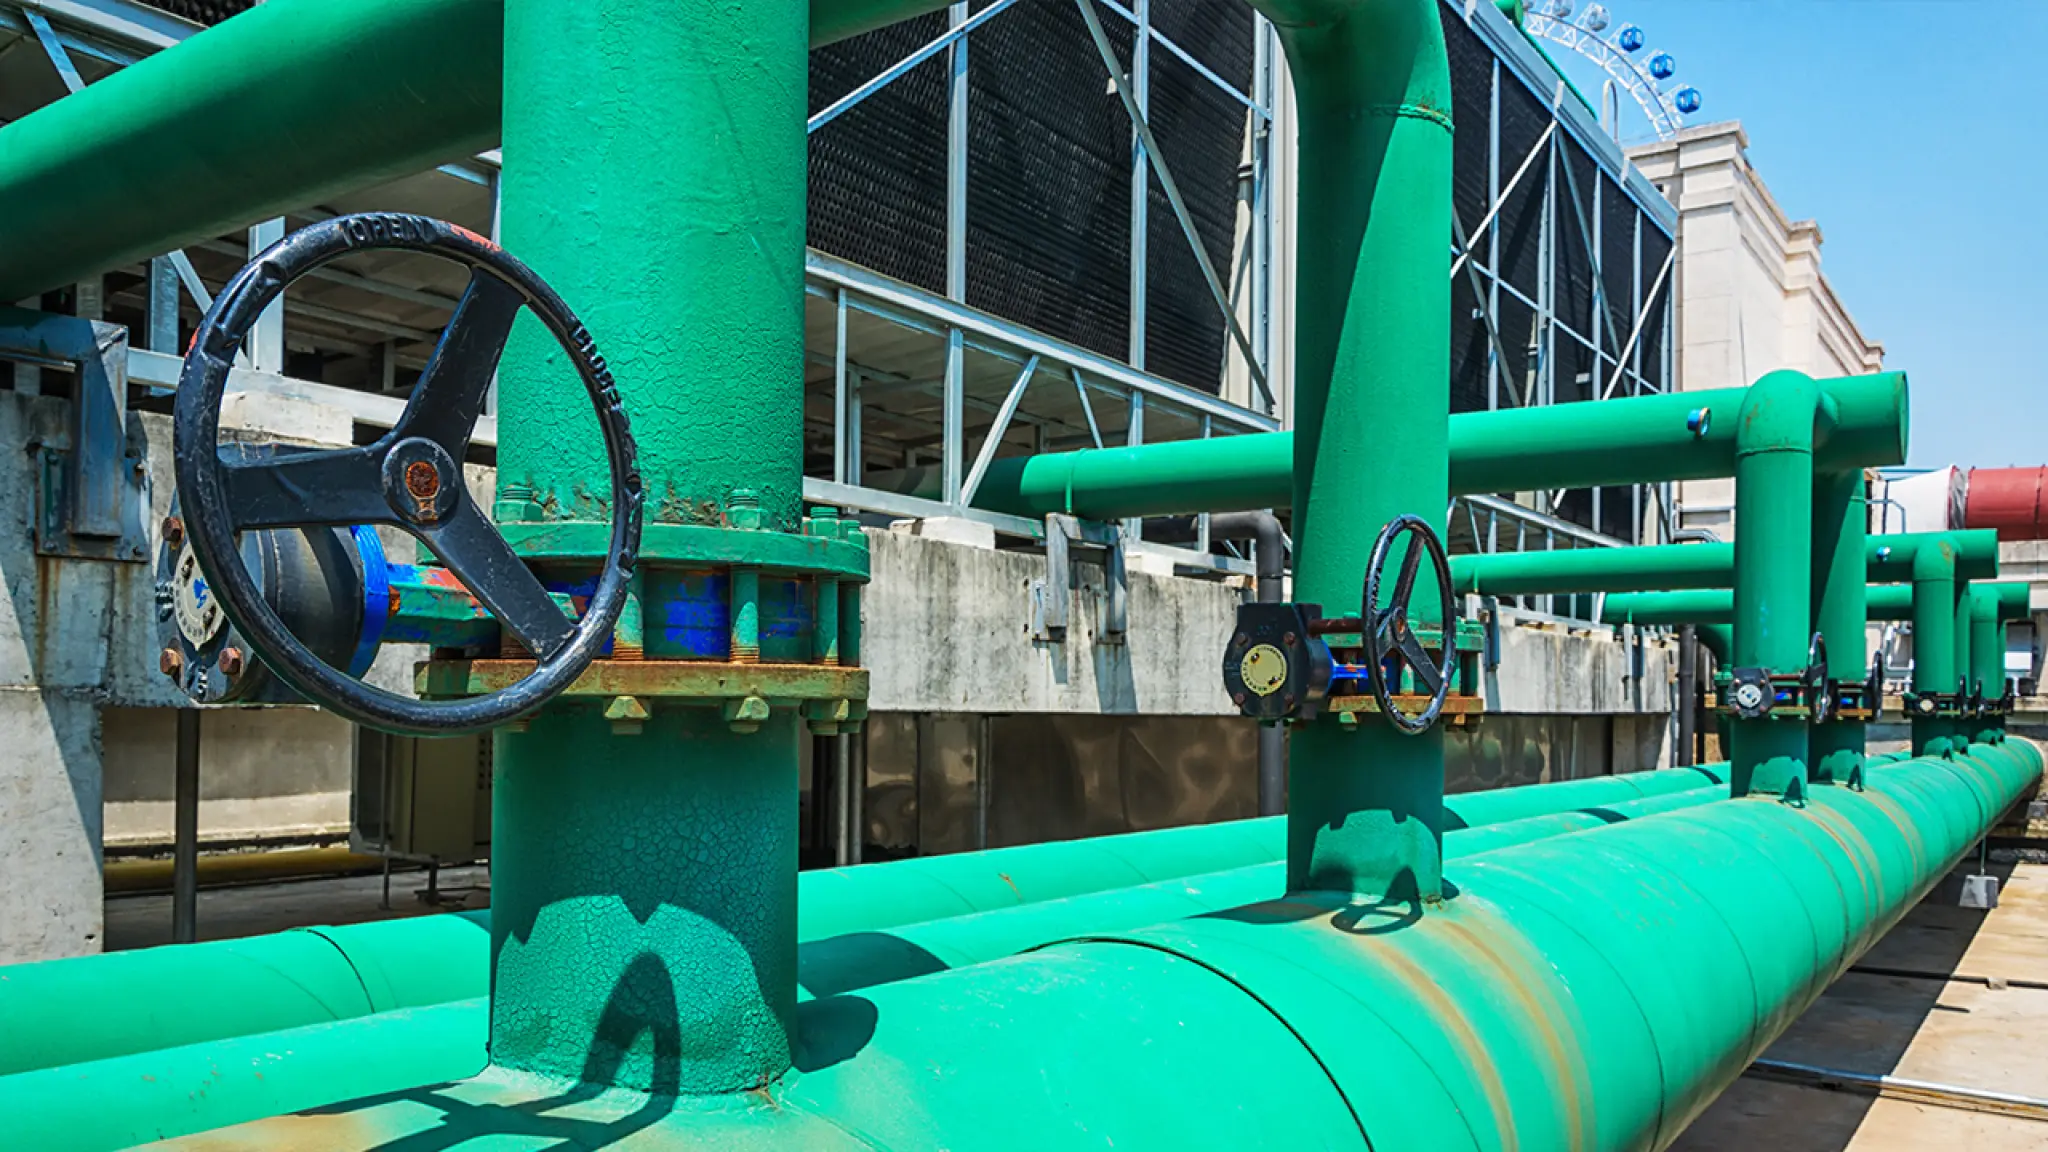
IE3 heavy-duty helical gear motors fitted with IP66 washdown protection seals and chemical-resistant coatings for agitators, clarifiers, and dosing pumps.
Multi-pole (4P–10P) 380V/660V heavy helical gear reducers engineered to absorb high shock loads, extreme thermal spikes, and severe vibration in steel rolling mills and overhead cranes.
Technical guidance for OEM buyers, electrical engineers, and factory sourcing specialists.
Need customized motor specifications, 3D CAD drawings, or bulk OEM factory pricing? Contact our application engineering team today to receive a complete technical catalog and tailored quotation.