Engineered for medical robotics, high-speed CNC machinery, AGV automation, and heavy industrial positioning systems.
 CE Certified
 Explosion-Proof
 Integrated Drive
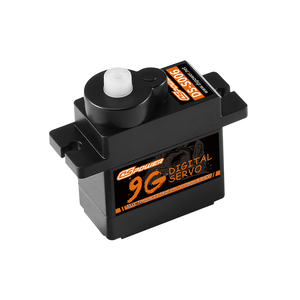 Micro Servo
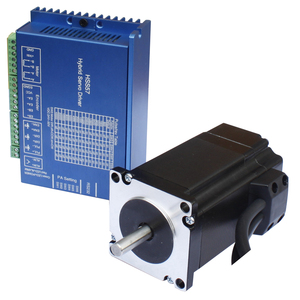 Closed Loop
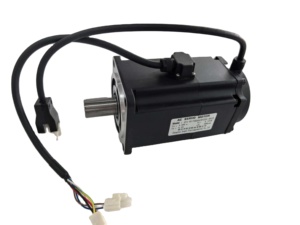 Electromagnetic Brake
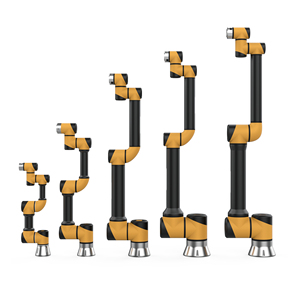 Robotic Joint
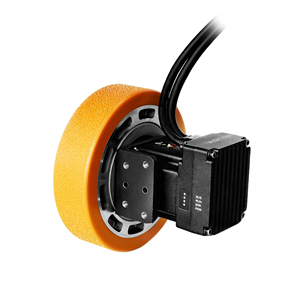 AGV / AMR Motion
In modern automated manufacturing, motion control reliability directly dictates total plant equipment effectiveness (OEE). A CE Certified Servo Drive is not merely a product bearing a regulatory stamp; it represents a comprehensive engineering framework ensuring electromagnetic compatibility (EMC), functional electrical safety, and mechanical isolation under strict European Directives.
For international original equipment manufacturers (OEMs) and factory automation integrators, sourcing servo systems from certified manufacturing facilities guarantees seamless integration into EU and North American production environments. Compliance with the Low Voltage Directive (LVD 2014/35/EU) and EMC Directive (2014/30/EU) guarantees that servo amplifiers operate reliably without emitting dynamic electrical noise that compromises nearby PLCs, sensors, or industrial communication networks.
Factories specializing in precision motion control architecture must validate every production batch through dynamic load testing, insulation resistance checks (HI-POT up to 2.5 kV AC), and thermal stress endurance. As industrial motion shifts toward direct-drive mechanisms and high-density permanent magnet synchronous motors (PMSM), CE certification provides the audited proof of safety required for heavy packaging, medical diagnostic apparatus, laser cutting, and robotic cell deployments.
A clear comparative analysis detailing how CE compliance affects electrical isolation, noise immunity, safety SIL levels, and lifespan under factory floor stress.
| Architecture & Performance Metric | Standard Uncertified Servo Drives | CE Certified Industrial Servo Drives |
|---|---|---|
| EMC Emission & Immunity | Unfiltered PWM output; susceptible to high-frequency ground noise and sensor feedback drops. | Integrated EMC Filter (EN 61800-3 Class C2/C3); dynamic ferrite core shielding and isolated fieldbus lines. |
| Functional Safety (STO) | External contactors required to drop main power; high latency safety interlocks. | Integrated Safe Torque Off (STO) certified to IEC 61800-5-2, SIL3 / PLe compliant. |
| Thermal & Overload Protection | Basic software thermal cutoff; risk of power stage (IGBT) catastrophic breakdown. | Multi-point NTC thermistor hardware integration; 300% peak overload for 3 seconds with active current limiting. |
| Enclosure & Vibration Seal | IP20 unsealed housing; plastic clips vulnerable to oil mist and vibration detachment. | IP54 / IP65 ruggedized enclosures; conformal coated PCBs (IEC 60068-2-6 shock & vibration validated). |
| Fieldbus Interoperability | Proprietary low-baud serial; isolated field communication unsupported. | EtherCAT, CANopen, RS485 (Modbus-RTU) with real-time sync jitter <1 μs. |
Founded with a commitment to engineering excellence, our enterprise has evolved into a global leader in factory automation, control panel manufacturing, and high-precision drive systems. Operating state-of-the-art SMT lines, automated motor winding facilities, and type-tested assembly plants, every drive system is built under stringent ISO 9001:2015 quality control protocols.
Our in-house capabilities span medium voltage drives (3.3 kV to 11 kV), high-speed AC servo drives, micro stepper drives, and custom collaborative robot joint actuators engineered for demanding global markets.
Global supply chain continuity demands robust local technical support. Backed by over 30 sales and application engineering service centers, our engineers provide application sizing, control cabinet thermal calculation, FAT (Factory Acceptance Testing), and remote commissioning support.
We work directly with machine builders and end-users to provide customized shaft dimensions, specialized fieldbus firmware, and integrated brake assemblies tailored specifically to target cycle-time goals.
Strategic procurement insights for industrial buyers, procurement directors, and chief automation engineers.
Eliminating centralized control cabinets is a primary cost-reduction driver. Integrated servo motors (combining driver, high-resolution encoder, and motor in a single IP65 housing) cut cabinet wiring volume by up to 70%, eliminate expensive shielded motor cables, and drastically minimize high-frequency radiation emissions on packaging and conveyor lines.
Autonomous Mobile Robots (AMRs) require low-voltage DC (24V–48V) high-torque servo wheel drives with direct heavy payload bearings. Sourcing integrated servo wheel actuators with CANopen or EtherCAT fieldbus interfaces enables sub-millimeter positioning, zero turn radius, and regenerative braking to prolong mobile robot battery runtimes.
Modern CE certified drives are incorporating edge telemetry. Real-time vibration Fourier transformation, dynamic winding temperature tracking, and encoder signal noise analysis enable predictive maintenance software to schedule service before catastrophic bearing or IGBT failure occurs on high-throughput assembly lines.
To carry the CE mark legally on industrial equipment, a servo drive system must comply with the Low Voltage Directive (LVD 2014/35/EU) governing electrical safety, insulation distances, and shock protection under EN 61800-5-1. Furthermore, it must satisfy the Electromagnetic Compatibility Directive (EMC 2014/30/EU) under EN 61800-3 standards, ensuring immunity against electrostatic discharge, fast transients, and limiting radiated radio-frequency interference.
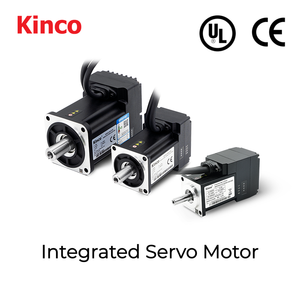
An integrated servo motor (such as the Kinco ISMK Series) merges the amplifier board and multi-turn absolute encoder directly onto the back bell of the motor frame. This eliminates separate driver cabinet mounting space, removes long shielded cable runs that create dV/dt motor insulation stress, reduces installation labor, and provides superior noise immunity since feedback signals do not travel along external plant cable trays.
Absolute encoders retain exact positional coordinates even during complete electrical power interruptions. When power is restored, the servo system immediately knows its precise mechanical axis position without executing a homing sequence. In medical diagnostic equipment or 6-axis collaborative robot joints, this prevents unexpected mechanical motion that could damage sensitive patient equipment, workpiece tools, or machine fixtures.
Yes. We supply customized servo motors featuring 100% pure copper wire windings, specialized shaft oil seals (IP65 / IP67), nickel-plated or stainless steel housings, and explosion-proof terminal boxes certified for hazardous ambient atmospheres. Additionally, conformal coated electronic drive boards protect power components against chemical mists, humidity, and conductive dust.
We supply comprehensive documentation packs including EPLAN schematics, EDS and ESI description files, CANopen dictionary tables, and sample function blocks for mainstream PLC software environments (including Siemens TIA Portal, Omron Sysmac Studio, Beckhoff TwinCAT, and Schneider Machine Expert). Our dedicated application engineering team supports FAT, communication protocol debugging, and axis parameter tuning remotely or on-site.
Looking to optimize your machine precision, achieve full CE compliance, or lower motion control unit costs? Connect directly with our application engineering team today for custom shaft drawings, torque curves, and bulk factory pricing.