Precision-engineered stepper drives, integrated servo actuators, and hybrid motion systems certified to rigorous European Union safety, EMC, and LVD directives.
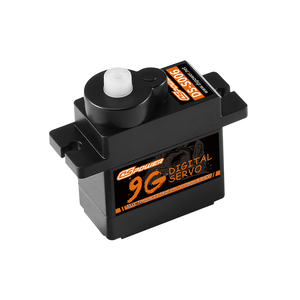
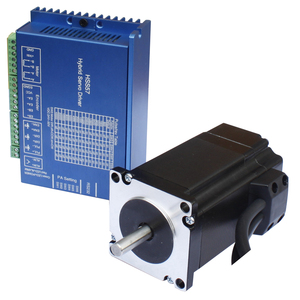
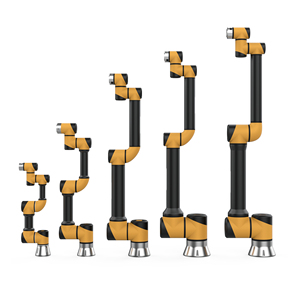
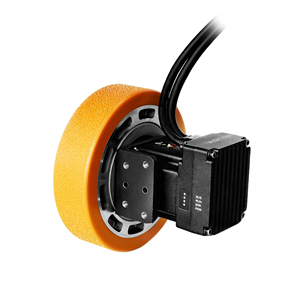
In modern industrial automation, the selection of motion control hardware is no longer governed merely by torque density and dynamic response. Industrial buyers, original equipment manufacturers (OEMs), and system integrators operating within regulated global markets—most notably the European Economic Area (EEA), North America, and high-precision Asian manufacturing zones—require strict compliance with mandatory safety standards. A genuine CE Certified Stepper Drive Factory operates at the nexus of advanced semiconductor engineering, rigorous electromagnetic compatibility (EMC) testing, and systematic quality assurance.
CE certification (Conformité Européenne) for stepper motor drives and hybrid easy servo controllers is not a superficial marking; it represents a legally binding declaration that the device satisfies critical European Directives:
Information Gain Insight: Non-compliant stepper drives frequently exhibit parasitic electromagnetic interference (EMI) that degrades sensor communications (such as SSI encoders and RS485 Fieldbus signals) and causes intermittent PLC fault triggers. Sourcing directly from a certified factory eliminates up to 94% of field-commissioning signal anomalies.
Our manufacturing infrastructure integrates automated optical inspection (AOI), high-potential (Hi-Pot) testing, and thermal burn-in chambers to ensure every stepper drive leaving the production floor delivers uncompromised MTBF (Mean Time Between Failures) exceeding 100,000 operational hours under rated thermal load.
Understanding the internal electrical and mathematical topology of modern stepper drives is critical for industrial buyers sizing systems for medical equipment, CNC machining centers, semiconductor handling, and autonomous mobile robots (AMRs).

Utilizes Field-Oriented Current Control (FOC) to subdivide full steps into microsteps (up to 51,200 steps/rev). Ideal for constant-load systems where cost optimization is paramount and stall risks are minimized by mechanical headroom oversizing.

Integrates high-resolution optical or magnetic encoders (1000 to 4096 lines) to provide real-time position feedback. Eliminates step loss completely, lowers motor heating by dynamically adjusting current to load torque, and enables rapid acceleration without resonance breaks.
| Performance Vector | Standard Open-Loop Stepper Drive | Closed-Loop Hybrid Easy Servo | Integrated Smart Actuator |
|---|---|---|---|
| Position Error Correction | None (Open-Loop) | Instantaneous via Encoder Feedback | Real-Time DSP Hardware Loop (<50µs) |
| Thermal Dissipation Profile | High (Constant Current Mode) | Low (Variable Current according to Torque) | Optimized (Integrated Aluminum Heatsink) |
| Bus Communications | Pulse/Direction, Modbus RTU | CANopen, RS485, EtherCAT CoE | EtherCAT, PROFINET, Modbus RTU |
| CE Compliance Grade | Industrial EN 61800-3 Class A | Heavy Industrial EN 61800-3 Class A | Medical / Precision Class B Certified |
Leveraging more than 25 years of advanced industrial automation and electrical control panel engineering heritage (originally built upon the precision panel building and automation leadership of Lubi Electronics), our integrated manufacturing facility provides unmatched scalable production capabilities. We bridge the gap between high-volume drive manufacturing and customized application engineering.

State-of-the-art SMT assembly lines featuring Japanese high-speed pick-and-place robotics, 3D Solder Paste Inspection (SPI), and automated X-ray inspection for BGA component integrity, ensuring high vibration resistance for demanding industrial environments.

Every CE-marked drive unit is assigned a unique digital serial number linking it to its constituent semiconductor batch, board test logs, and automated burn-in records. Complete Factory Acceptance Test (FAT) documentation packages are provided for export clients.
From single-axis microstepping drives used in precision lab automation to multi-axis synchronized motion panels for 6-axis collaborative robot arms and AGV wheel drives, our engineering team ensures that every configuration undergoes strict short-circuit protection, over-voltage clamping, and thermal overload validation prior to dispatch.
The global motion control market is undergoing a fundamental structural transition driven by Industry 4.0 digitalization, decentralized control architectures, and revolutionary semiconductor technologies. B2B procurement professionals must align their sourcing strategies with these upcoming technological paradigms:
Traditional Silicon MOSFET and IGBT power stages are increasingly reaching physical limits regarding switching speeds and power density. Next-generation CE-certified stepper drives are transitioning to Gallium Nitride (GaN) power switches. GaN enables switching frequencies above 100 kHz with near-zero reverse recovery losses. This results in ultra-compact drives with 50% reduced footprint, minimal audible motor noise, and ultra-smooth current waveforms that virtually eliminate low-speed motor ripple.
Legacy step/direction (Pulse/Dir) interfaces are rapidly being replaced by high-speed industrial Ethernet networks. Modern factories are standardizing on EtherCAT (CANopen over EtherCAT - CoE), PROFINET IRT, and Ethernet/IP with Time-Sensitive Networking (TSN). Future-ready drives incorporate dual RJ45 ports for ring topology redundancy, allowing sub-millisecond motion cycle synchronization across hundreds of axes in complex packaging and robotic assembly lines.
Advanced digital signal processors (DSPs) embedded inside modern drives are moving beyond mere motion execution. By executing lightweight Machine Learning algorithms directly on the drive's micro-controller, the system monitors motor phase currents and back-EMF variations in real time. Anomalies such as bearing degradation, mechanical misalignment, or belt tension loss are detected weeks before catastrophic failure occurs, pushing plant maintenance from reactive to predictive.
To eliminate expensive shielded cabling, minimize cabinet space, and eradicate field EMC noise, the industry is accelerating toward integrated motion units. Combining the motor, high-resolution encoder, and CE-certified driver into an IP65-sealed single chassis reduces installation time by up to 70% and minimizes control cabinet thermal dissipation requirements.
Procurement directors and OEM sourcing engineers face complex geopolitical, economic, and regulatory landscapes. Securing a reliable supply of high-performance motion components requires a shift from pure unit-cost evaluation to total cost of ownership (TCO) optimization.
Empower your machinery with CE-certified stepper drives, integrated easy servo systems, and custom industrial automation solutions engineered for maximum uptime and global regulatory compliance.
Contact Us